 +86 18310268158
Aluminum Stamping: How It Differs from Steel
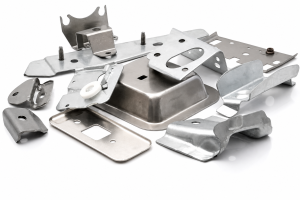
Aluminum stamping runs on the same presses as steel, but the material changes four things. Force, tooling, springback and surface finish all shift when the sheet turns aluminum. Get those four wrong and the part fails at tryout. Get them right and the part costs less to form than its steel twin. Our factory in Nanpi, Hebei, has stamped metal since 1999. This guide lists the differences, with the rule we apply on every job. For the background on why we stamp at all, see our post on the custom aluminum fabrication experience.
Why Stamp Aluminum in the First Place
- Weight: about one third of steel at the same size.
- Conductivity: heat and electricity move freely.
- Corrosion: the oxide layer protects the part by itself.
- Recyclability: scrap goes back into the melt, full value.
Automotive brackets, electrical enclosures and heat sink housings are classic aluminum stamping jobs. The part is light where the design needs light. It conducts where the design needs to conduct. If your steel version fights both, the material is the wrong answer.
What Changes When the Sheet Is Aluminum
| Factor | Steel | Aluminum |
|---|---|---|
| Forming force | Baseline | Lower, often well under half |
| Die wear | Moderate | Low, but galling risk |
| Springback | Predictable per grade | Higher on 5052 and 6061 |
| Surface | Tough skin | Marks easily |
| Material price | Baseline | Higher per kilogram |
Read the table left to right and the message is simple. Aluminum is easier to form but easier to mar. The press works less; the handling works more. Your die and your fixtures must protect the surface from the first hit.
Tonnage: Less Force, Bigger Margin
Aluminum needs less force than steel at the same thickness. A part that needs 200T in 2mm steel can often run under 100T in 2mm aluminum. The smaller press handles the job, and the cycle stays fast. Our line holds 40+ presses from 60T to 400T. The aluminum job sits on the small machines. The big ones run steel. The matching rules, part size to tonnage, are in our stamping capacity guide. Ask any supplier which press your aluminum part will run on. The answer separates a planner from a guesser.
Tooling: Coatings and Release
- Work-hardening alloys want a coated die face, not bare steel.
- Release is applied on 5052 and 6061 jobs, checked per hit.
- Die lips are polished to keep the part edge clean.
- The tryout log records coating condition, not just part size.
Galling is the failure mode: aluminum sticks to the die and tears. It starts as a smear and ends as a rejected lot. Coating, release and a polished lip keep the bond down. The die life and maintenance rules are on our metal stamping die page. They apply to aluminum with one extra line. The coating is part of the maintenance schedule.
Springback: The Number That Moves per Alloy
Every bend opens back a little after the punch leaves. Springback is larger on the stronger alloys. 1100 bends almost like steel. 5052 and 6061 open back more, and the angle must be over-formed to compensate. We store the compensation per alloy and per thickness, and we update it from the measured tryout. If the drawing names the alloy, the angle target follows it. The default classes and the tighter ones we hold are listed in sheet metal tolerance standards. Do not send a bend angle with no alloy behind it. The angle is not a number until the material is named.
Surface: Protect It From the First Nest
- Protective film on the coil, kept on through nesting.
- No bare edge to bare edge contact in the nest.
- Die contact faces kept polished and clean per shift.
- Finished parts racked, not stacked, on the shop floor.
Steel forgives a scratch; aluminum shows it to the customer. The protection starts before the cut, at the coil. It ends at the packing line, not before. Which finish the part wears after stamping is a separate decision. Our guide to surface treatment for custom metal parts covers it. Anodize, powder coat or bare: pick it once, on the drawing.
Cost: More Material, Less Forming
The two lines move in opposite directions. Aluminum sheet costs more per kilogram than mild steel. The forming cost per part is lower, because the force is lower and the die wears slower. At volume, the forming saving grows with every piece. The material premium stays flat. Our post on metal stamping cost splits the unit price into material, labor, overhead and margin. Run your part both ways, steel and aluminum, and compare the two lines separately. The winner is not always the cheaper sheet.
Common Alloys, Plainly
- 1100: the soft workhorse, easiest to form, low strength.
- 3003: general purpose with better corrosion resistance.
- 5052: medium strength, the marine and automotive pick.
- 6061: the strong one, weldable, higher springback.
The alloy sets the strength, the formability and the springback at once. Name it on the drawing and the price follows it. Mixing 5052 and 6061 in one lot is a defect, not a preference. We check the mill certificate against the drawing at intake, on every coil. That one check is the reason the alloy on your part is the alloy you asked for.
When Stamping and Casting Meet
Some assemblies pair a cast aluminum body with stamped aluminum hardware. The cast part carries the structure; the stamped part carries the function. Holes, clips and brackets get stamped while the housing gets cast. The two parts arrive from the same factory, on the same schedule. One of those combinations is in our case file. It was built and shipped as a single assembly: aluminum castings and stamped parts. If your product has both shapes, send both drawings. The quote comes as one, not two.
How We Run Aluminum
- 40+ presses from 60T to 400T, aluminum on the small end.
- Coated die faces and per-hit release on the work-hardening alloys.
- 6kW laser for the blanks, film on the sheet through nesting.
- Mill certificate checked at intake, part measured at every stage.
- Since 1999: 70,000+ different types of custom metal parts, aluminum included.
The list is the check list, applied to our own floor. Aluminum stamping is not a separate factory. It is the same line with four adjustments: less force, a coated die, a stored springback and a protected surface. Send the drawing and the alloy, and the quote names the press and the finish. That is the whole conversation.
Frequently Asked Questions
Is aluminum harder to stamp than steel?
The press makes it easier: less force, slower die wear. The rest is harder: springback, galling and surface marks all need more control. The material is gentler on the machine and stricter on the process.
Which aluminum alloys do you stamp?
1100, 3003, 5052 and 6061 are the daily four. The alloy sets strength and springback, so name it on the drawing. We confirm the stock and the mill before the quote is final.
What thickness of aluminum can you stamp?
From thin gauge for clips to several millimeters for brackets. The thickness sets the tonnage and the tooling. Send the part and we name the press and the die in the reply.
Does stamped aluminum need surface treatment?
Bare anodized aluminum holds up outdoors. Powder coat adds color and thickness. The decision belongs on the drawing, picked once. We apply the finish in-house after stamping.
Is aluminum stamping more expensive than steel?
The material line is higher. The forming line is lower, and it falls with volume. Run both metals against your part and compare line by line. The total, not the sheet price, decides.
Start Your Aluminum Stamping Project
Send your drawing — an 8-hour quote and material check.
WhatsApp: +86 183 1026 8158 | Email: alina@xinjiuxinji.com
Or request a quote online.